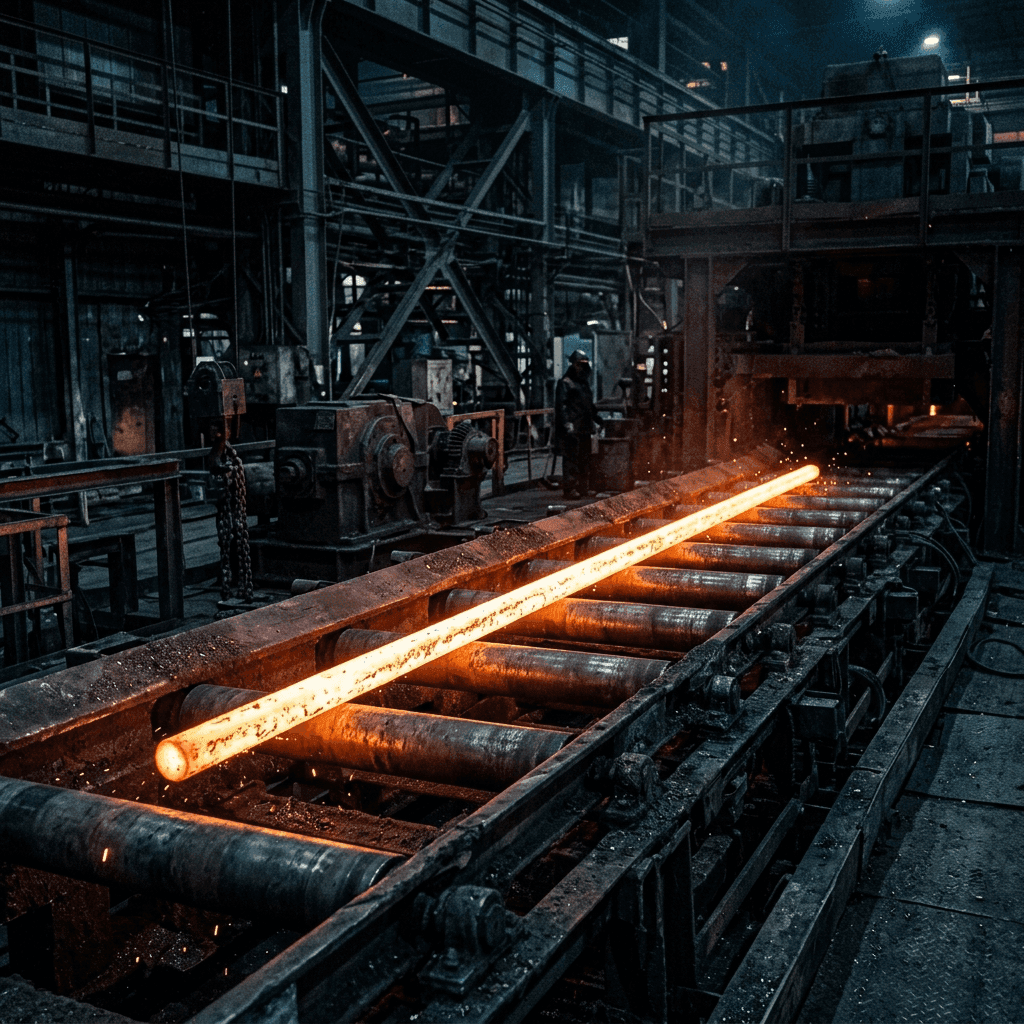
INFRASTRUCTURE.
Advanced infrastructure, controlled processes, and precision engineering for consistent steel quality.
STATE-OF-THE-ART
MANUFACTURING
INFRASTRUCTURE.
“Equipped with advanced manufacturing technology, modern machinery, and comprehensive testing facilities engineered to ensure precision, efficiency, and consistent product quality.”
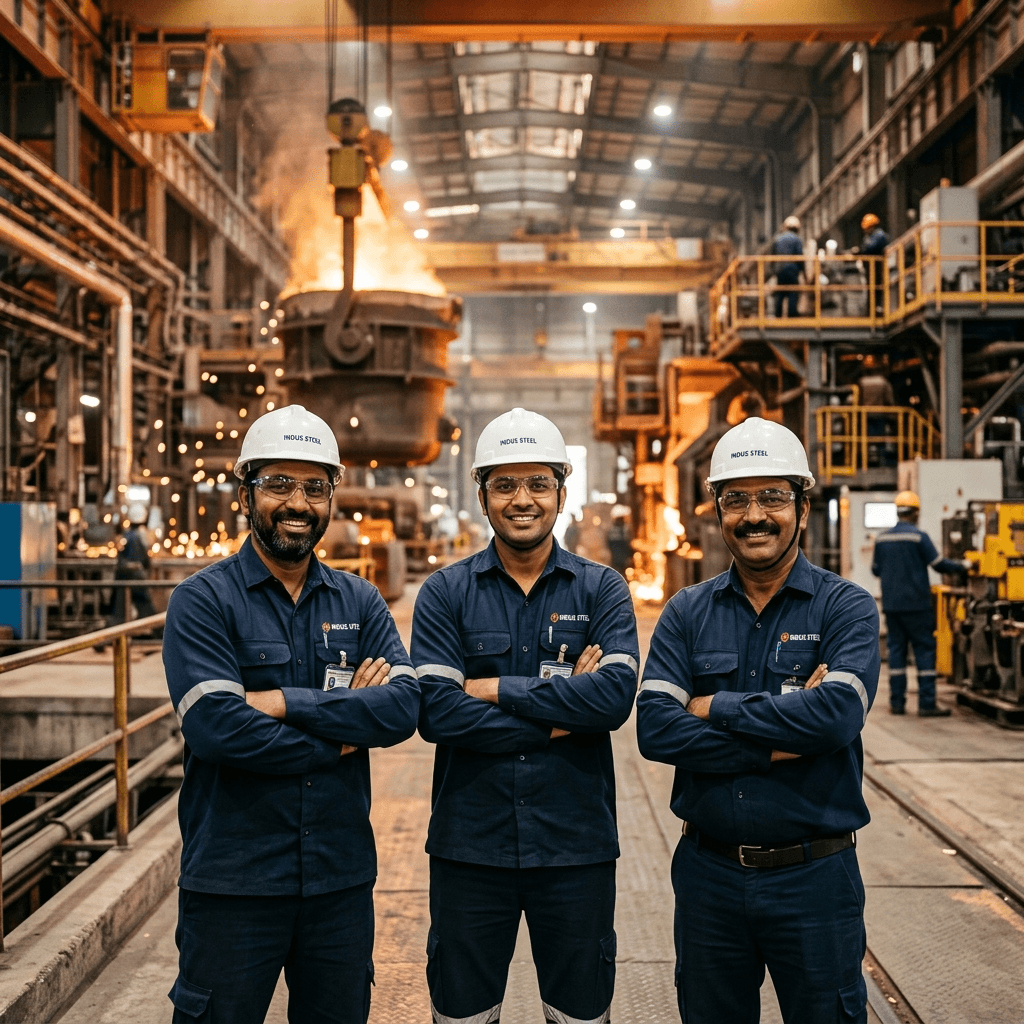
At Subhlaxmi Steel and Alloys Pvt. Ltd., our world-class infrastructure forms the foundation of our commitment to delivering premium-quality stainless steel, alloy steel, carbon steel, and special metal products. Our integrated plant setup enables us to manage every stage of production — from incoming raw material inspection to final product dispatch — under strict quality control.
GUJARAT, INDIA
ADVANCED PRODUCTION SYSTEMS
Modern melting, refining, and rolling equipment supporting a wide range of stainless steel and alloy grades.
INTEGRATED PLANT SETUP
Complete operational management from raw material sorting to final packaging under strict quality supervision.
CONTINUOUS INFRASTRUCTURE UPGRADES
Regular equipment and technology upgrades to improve production efficiency and maintain product consistency.
GLOBAL STANDARDS COMPLIANCE
Strict process control ensuring products conform to international specifications and demanding OEM standards.
ADVANCED
MACHINERY &
EQUIPMENT.
Equipped with high-performance manufacturing technology, modern melting furnaces, multi-stand rolling lines, and computerized thermal processing units.
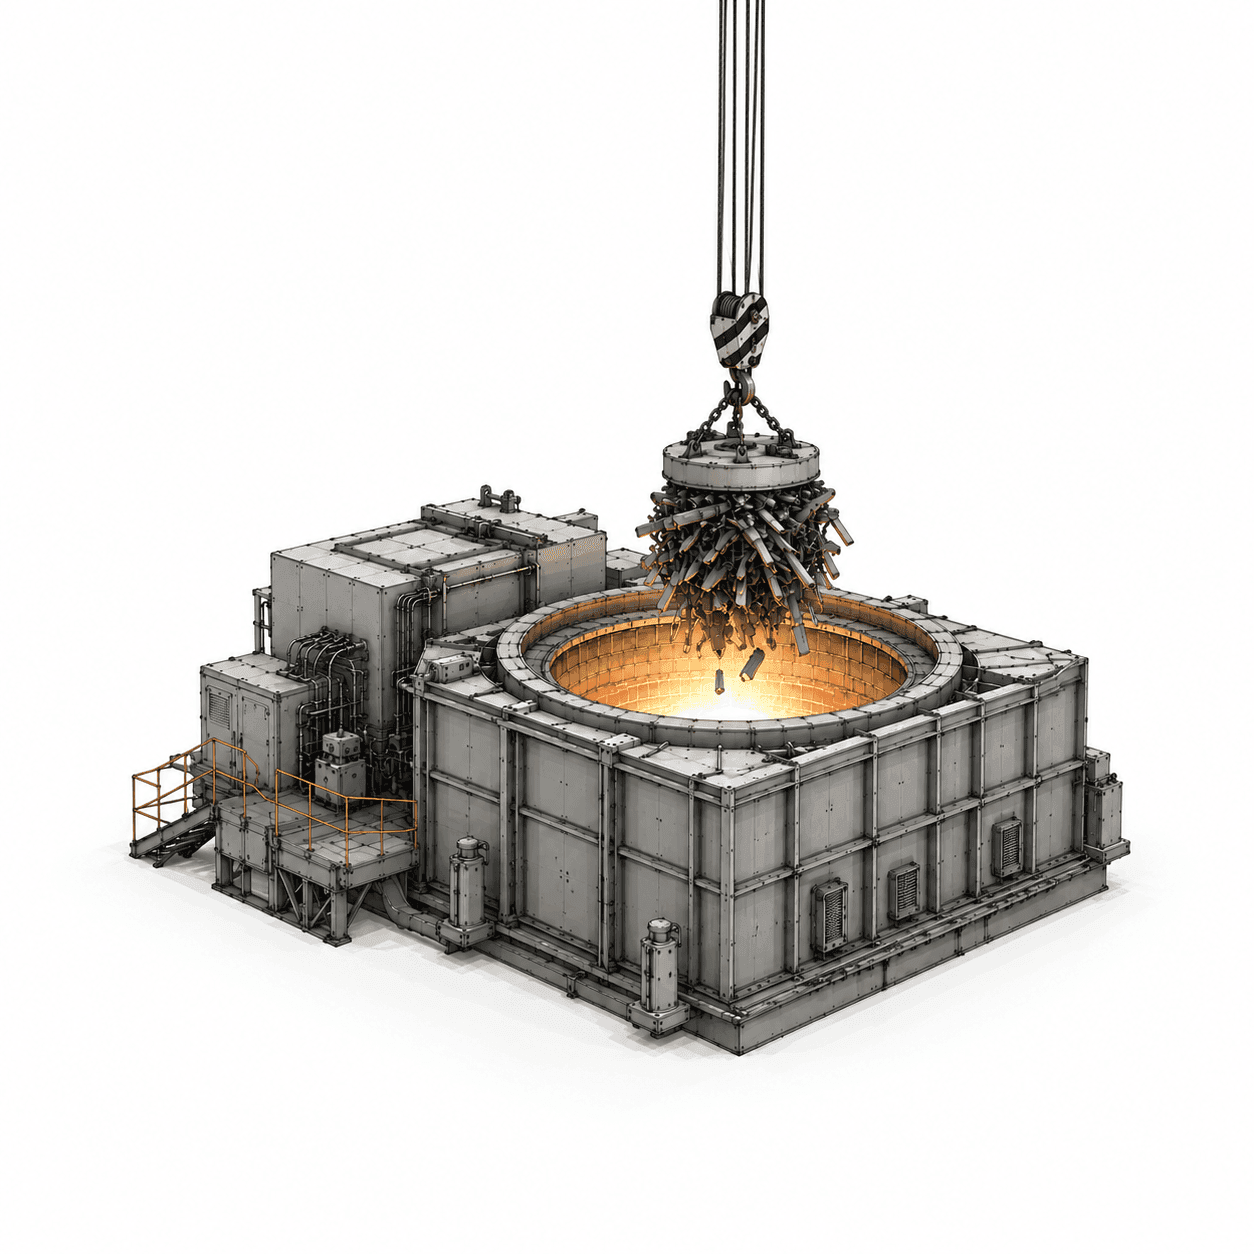
ELECTRIC INDUCTION FURNACE (EIF)
High-efficiency Electric Induction Furnace (EIF) melting with precise thermal control, ensuring clean liquid metal and exact chemical composition.
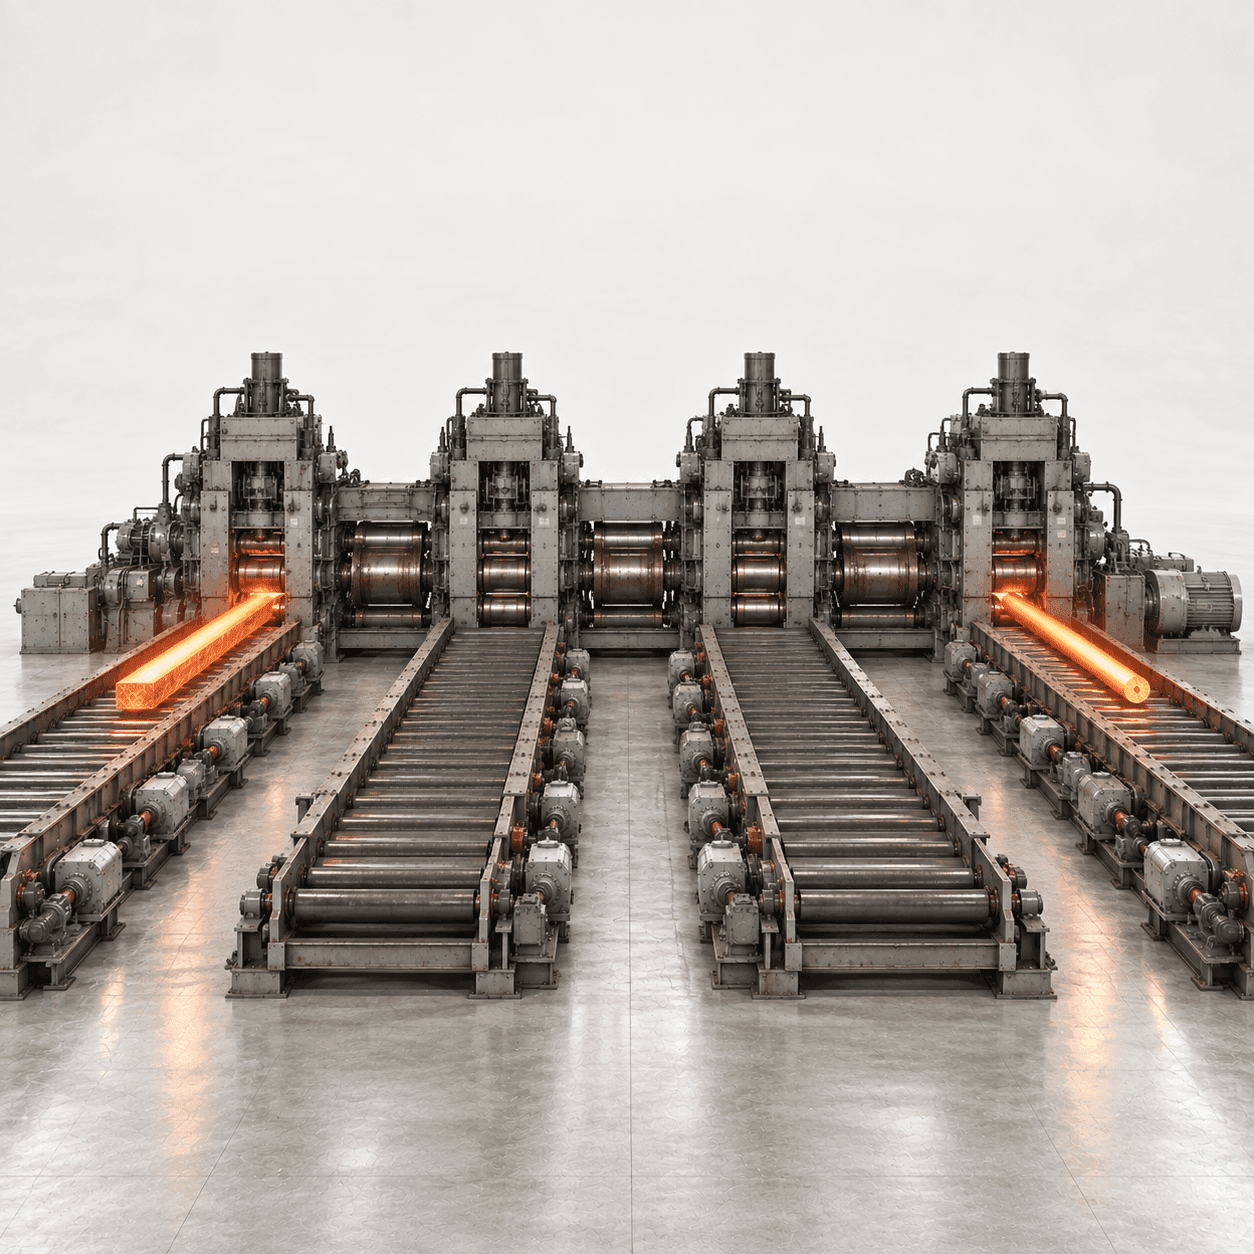
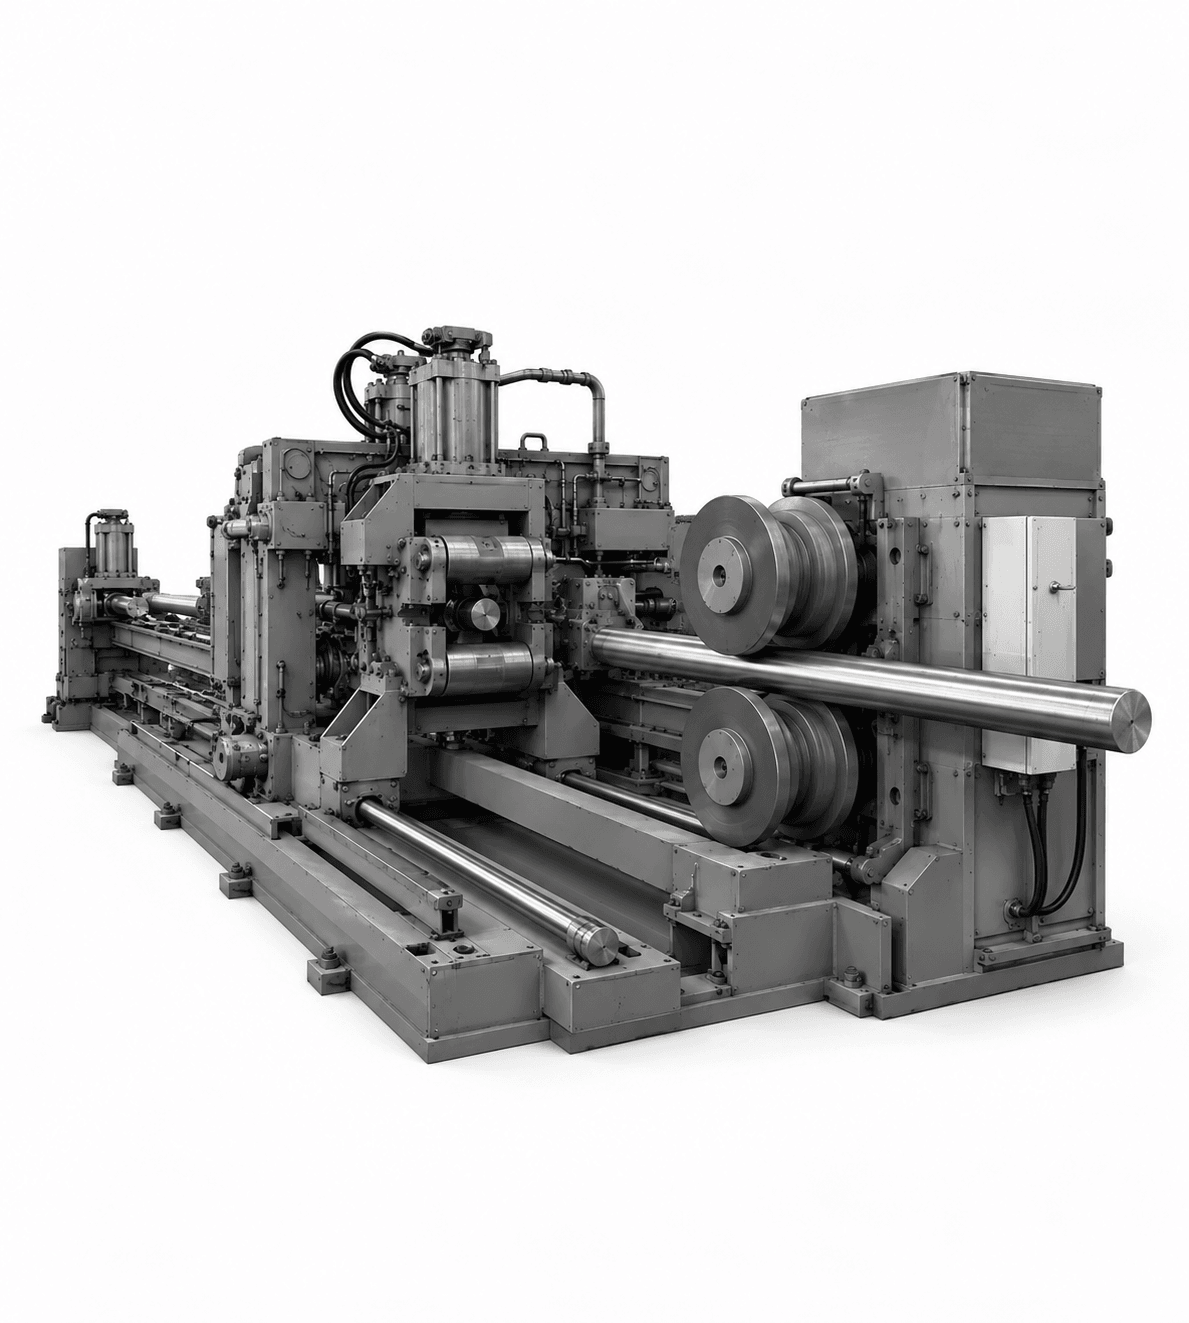
HOT ROLLING MILL
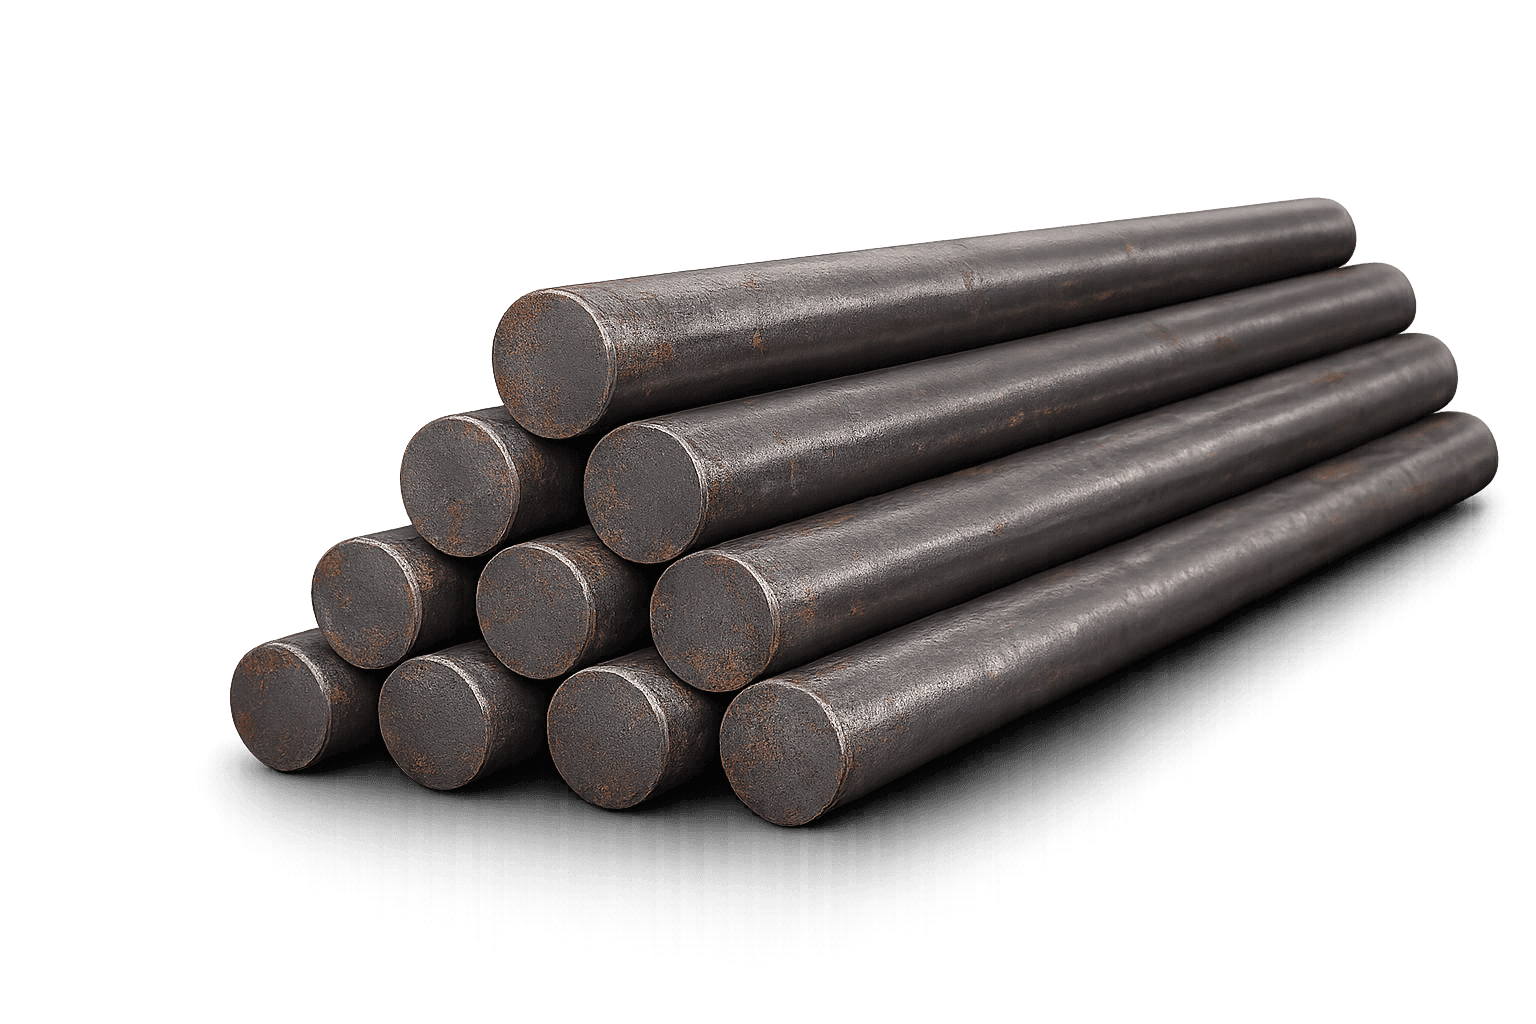
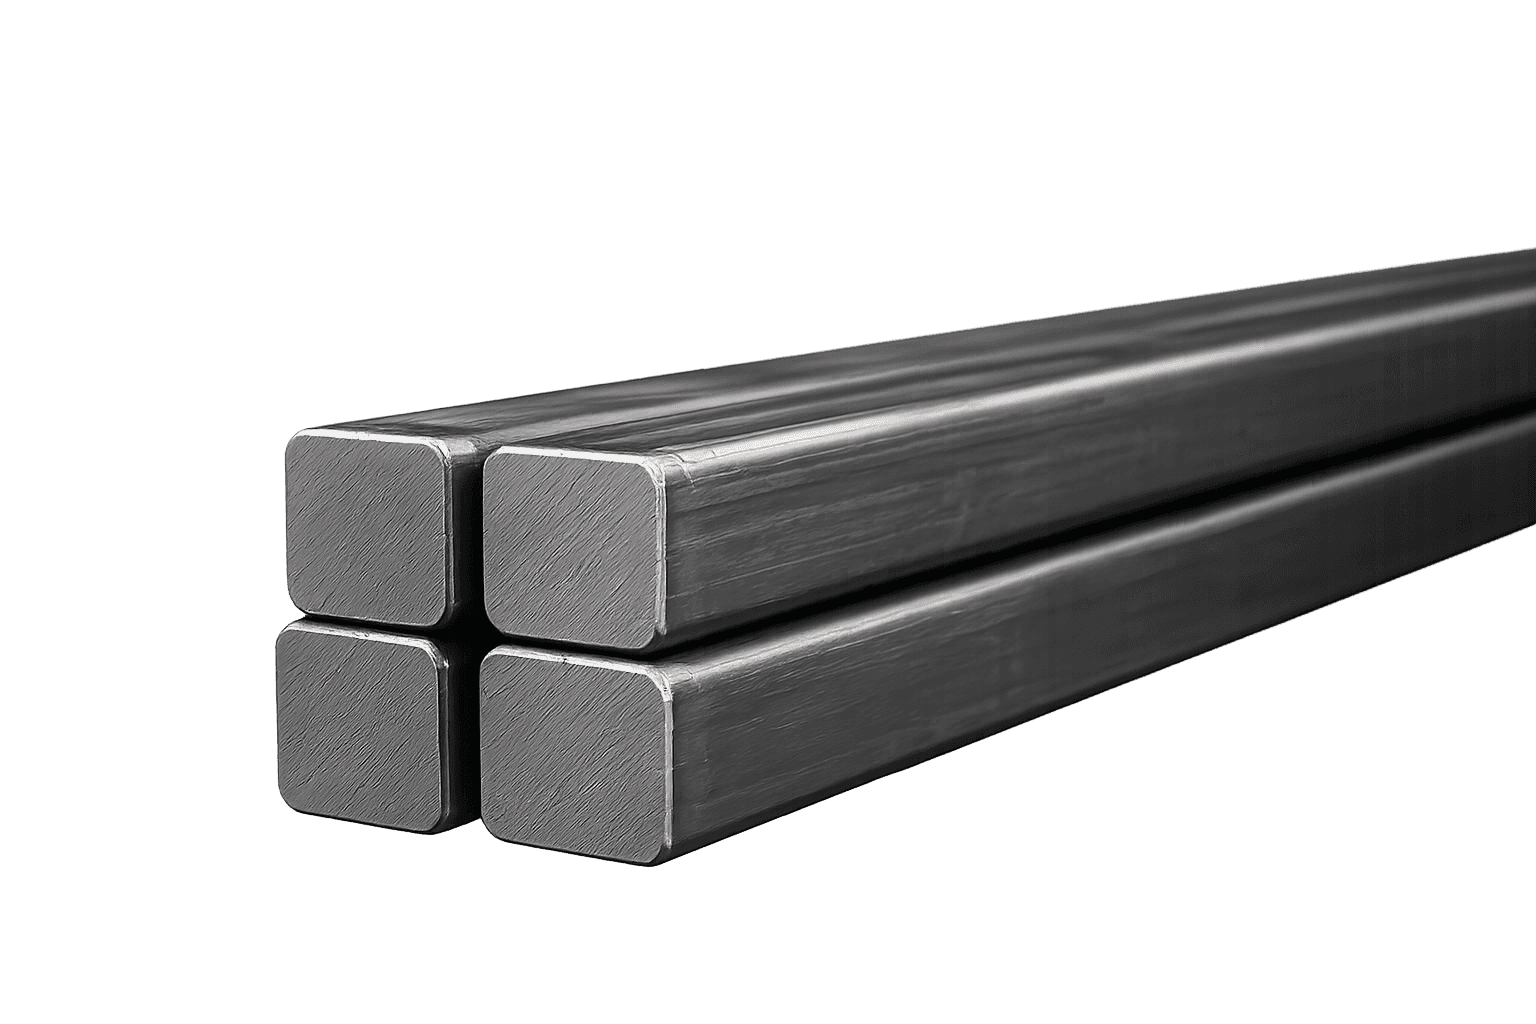
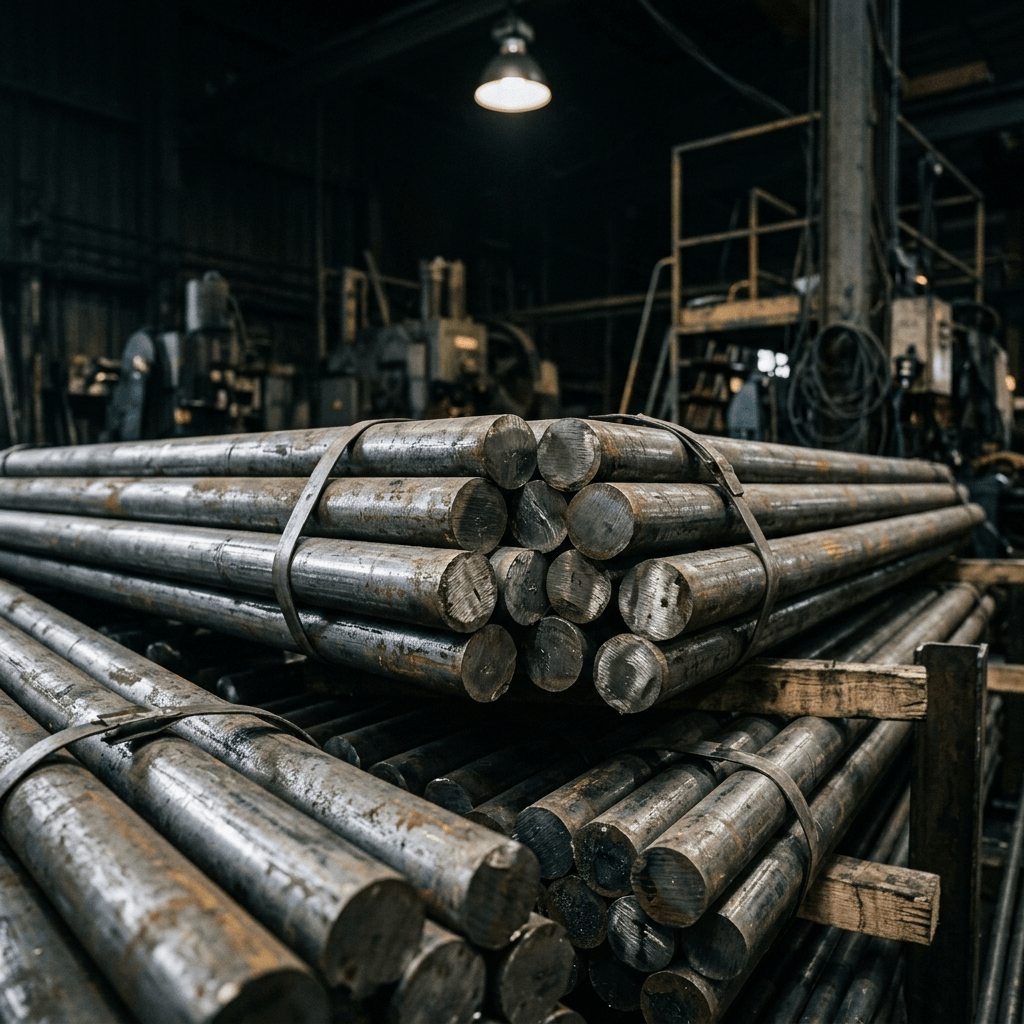
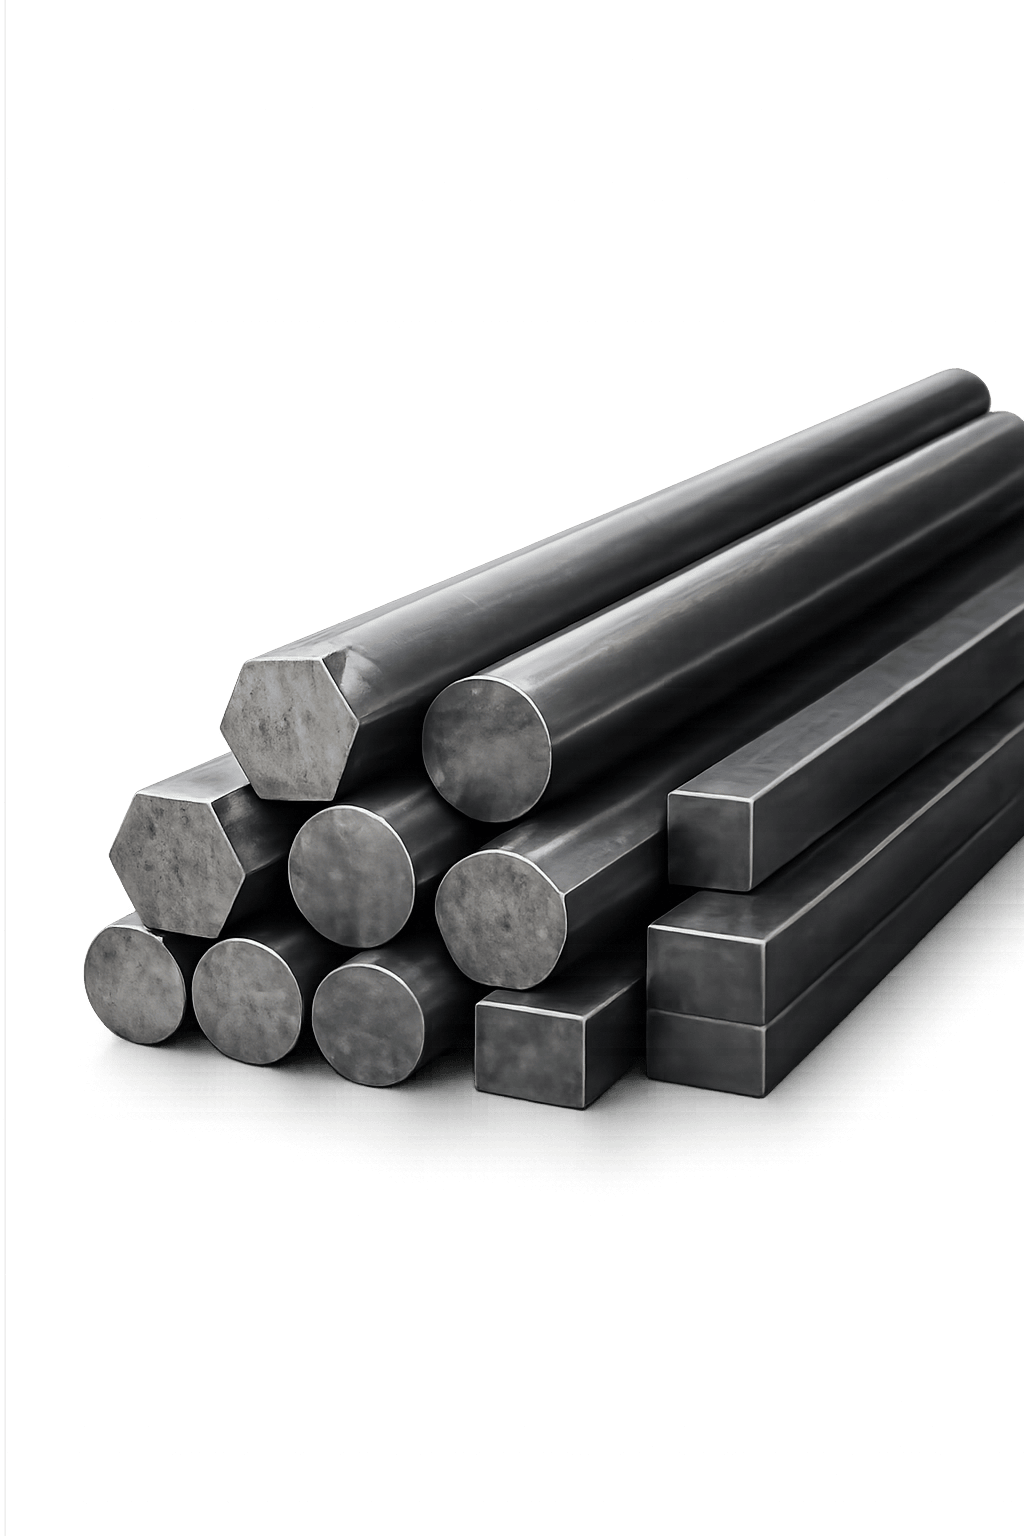
Multi-stand rolling setup producing round bars (16mm to 130mm) and RCS with uniform dimensions and structural integrity.
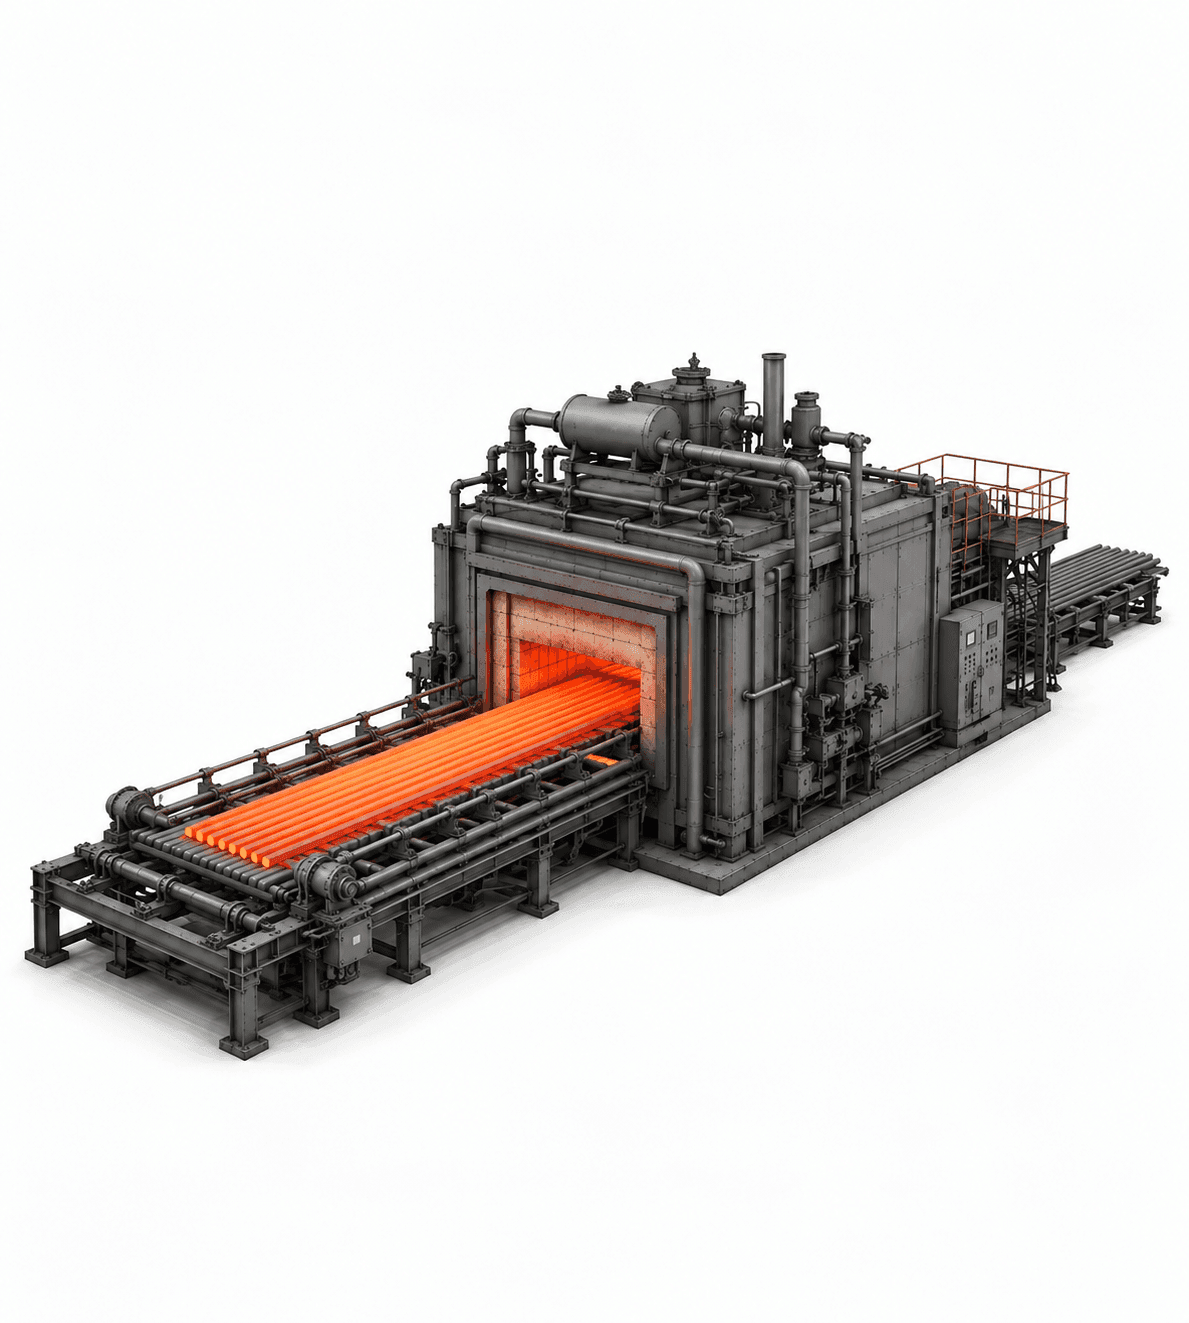
HEAT TREATMENT FURNACES
Computerized thermal units providing annealing, normalizing, hardening, and tempering for optimal mechanical properties.
FINISHING & HANDLING SYSTEMS
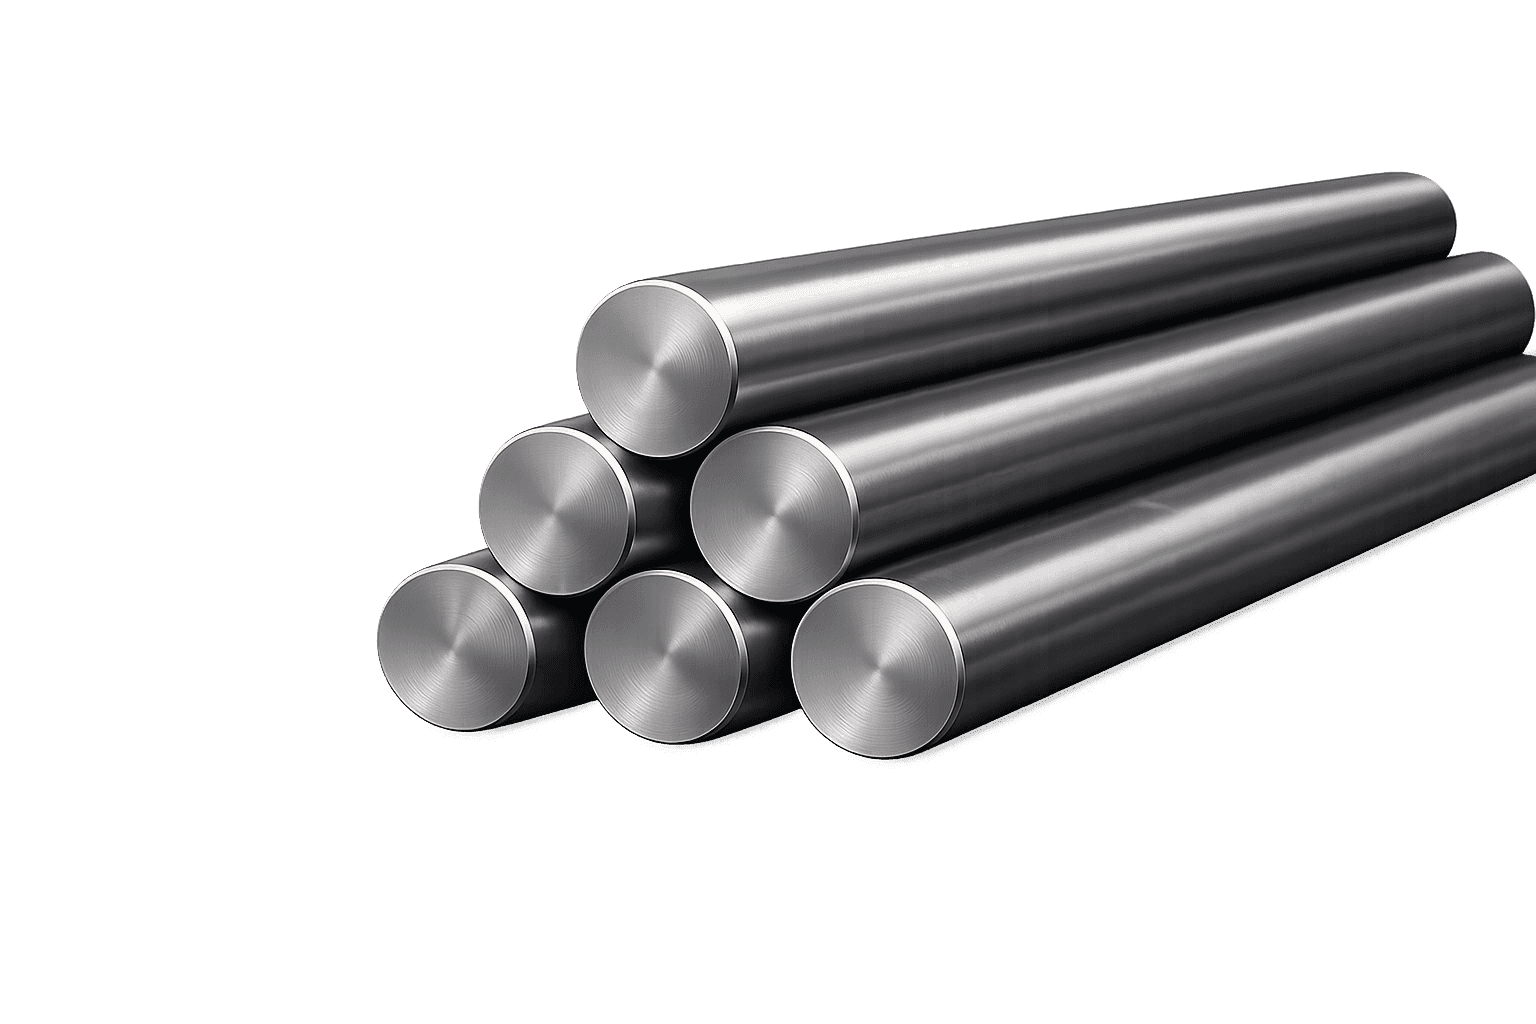
Centerless bar peeling, grinding, straightening, and automated material handling for superior surface finish and precision.
ELECTRIC INDUCTION FURNACE (EIF)
High-efficiency Electric Induction Furnace (EIF) melting with precise thermal control, ensuring clean liquid metal and exact chemical composition.
HOT ROLLING MILL
Multi-stand rolling setup producing round bars (16mm to 130mm) and RCS with uniform dimensions and structural integrity.
HEAT TREATMENT FURNACES
Computerized thermal units providing annealing, normalizing, hardening, and tempering for optimal mechanical properties.
FINISHING & HANDLING SYSTEMS
Centerless bar peeling, grinding, straightening, and automated material handling for superior surface finish and precision.
100% IN-HOUSE PROCESS CONTROL
From raw scrap sorting & induction melting to 13-stage dispatch verification under ISO 9001:2015.
OUR
MANUFACTURINGPROCESS
A well-defined 13-stage metallurgical process, powered by technology and engineering expertise, to deliver high-quality alloy steel products.
MTC EN 10204 3.1 CERTIFIED
Complete material traceability with certified chemical heat analysis & mechanical property reports.
100% VOLUMETRIC UT & MPI TESTED
Immersion Ultrasonic Testing and Magnetic Particle Inspection surface flaw clearance for every bar.
Raw Material Selection & Audit
High-grade stainless steel scrap and alloy additions undergo strict grade verification prior to furnace charging.
Electric Induction Furnace Melting
Selected raw materials are melted under computer-monitored operating parameters and precise pyrometry control.
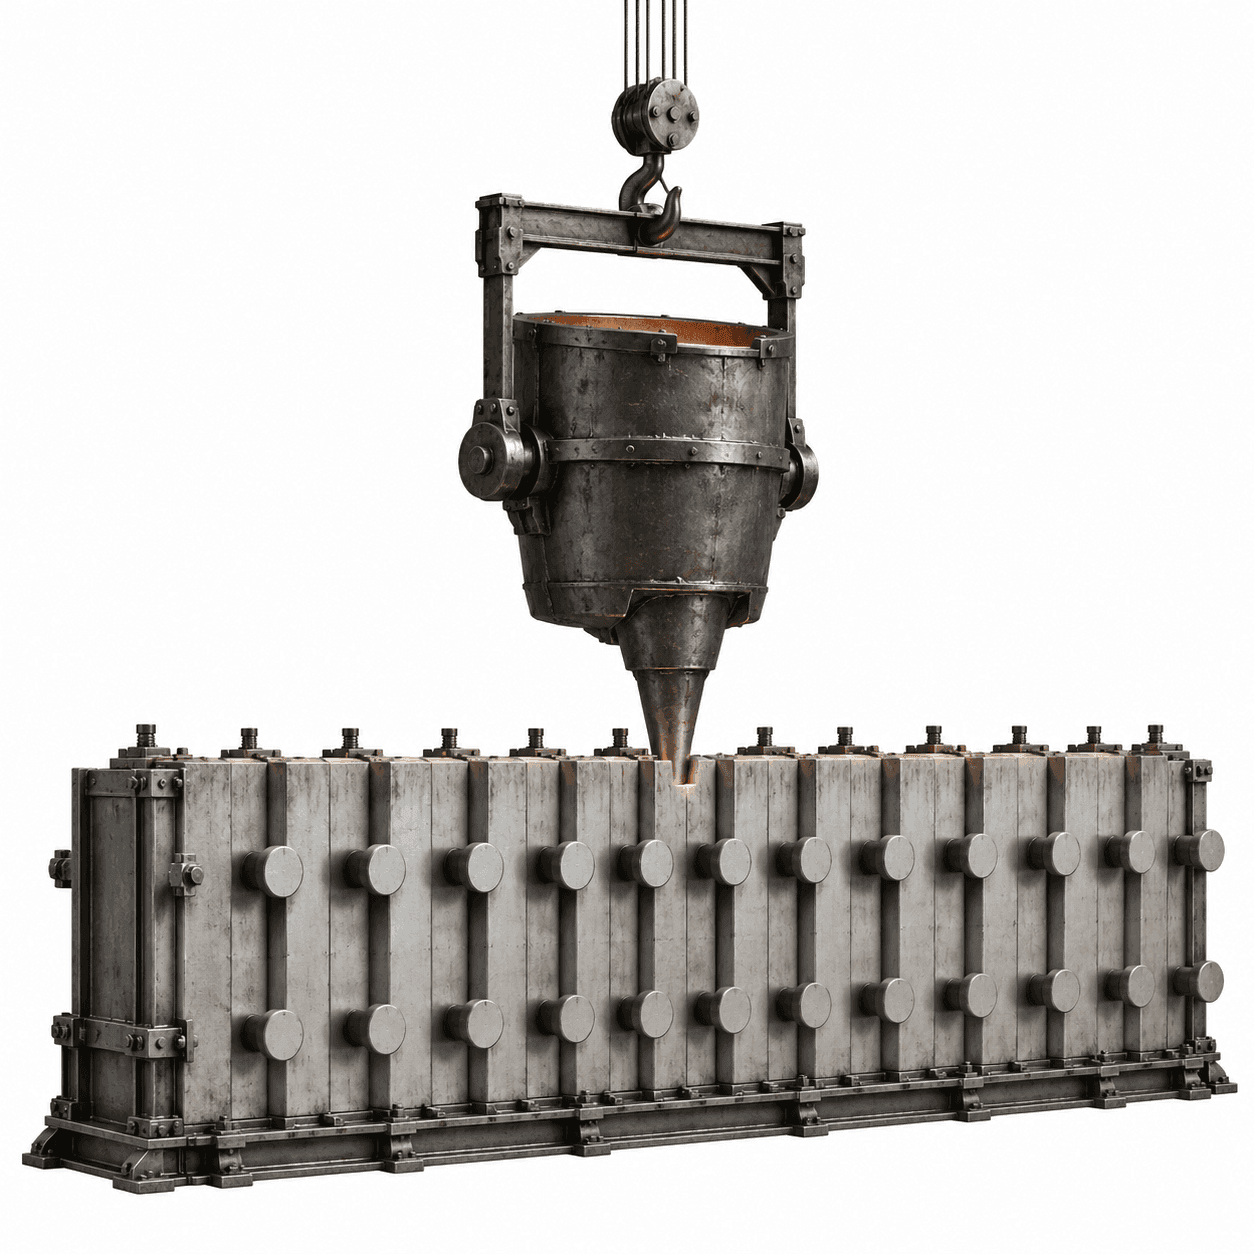
Bottom-Poured Ingot Casting
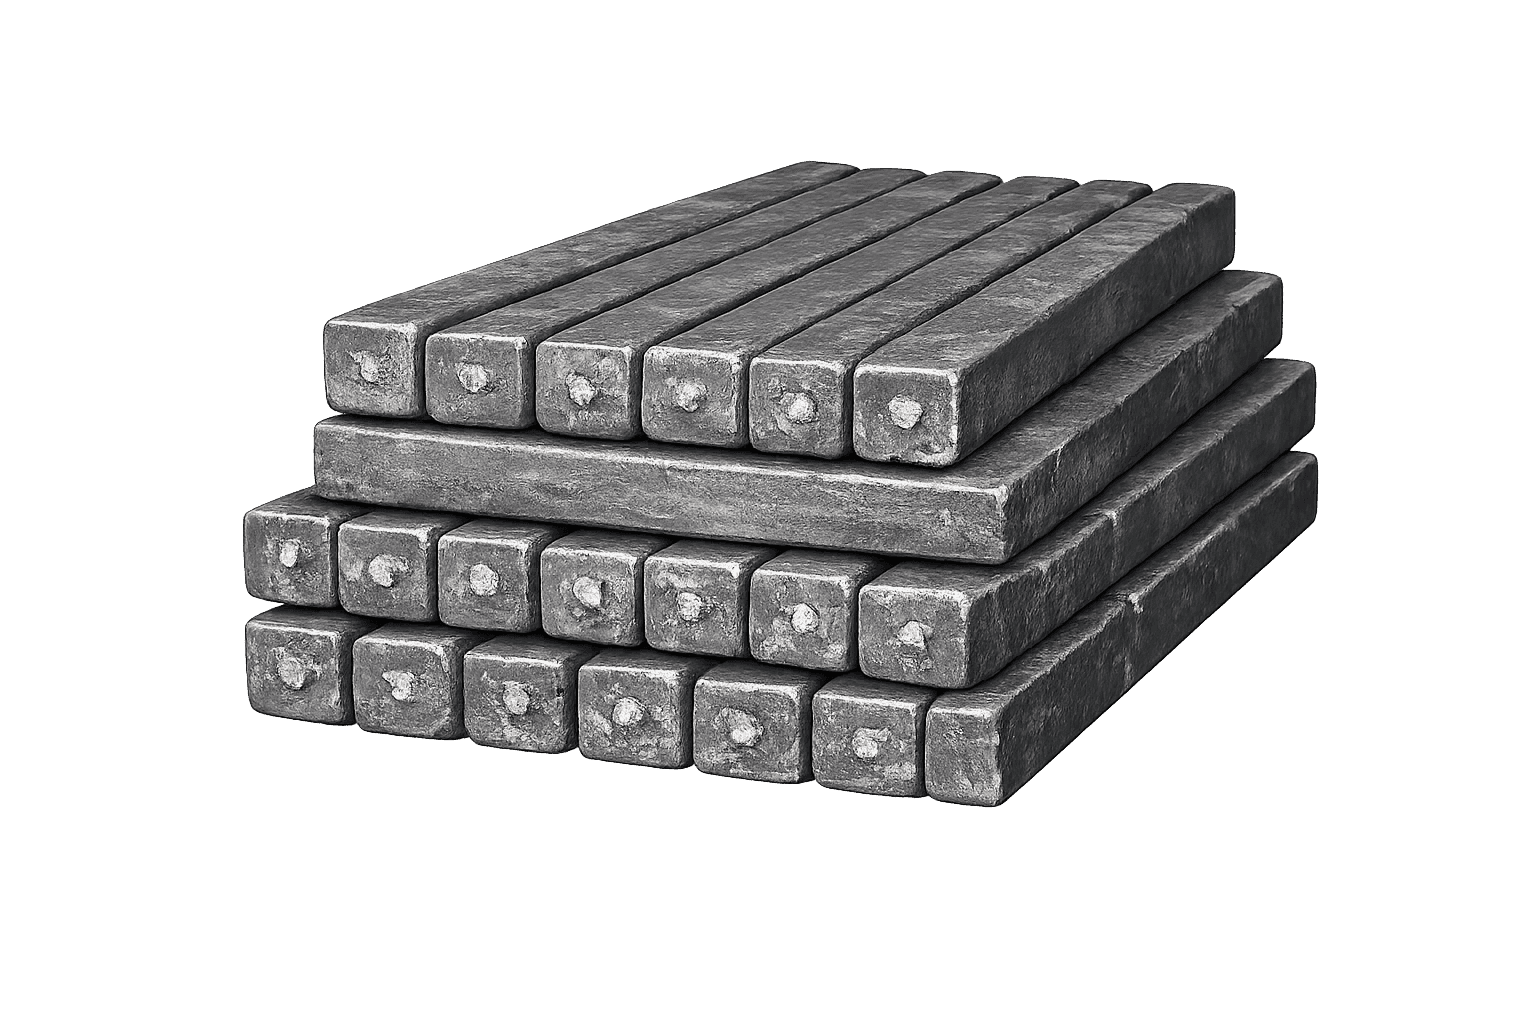
Refined molten metal is cast into molds under controlled bottom-pouring conditions for uniform grain structure.
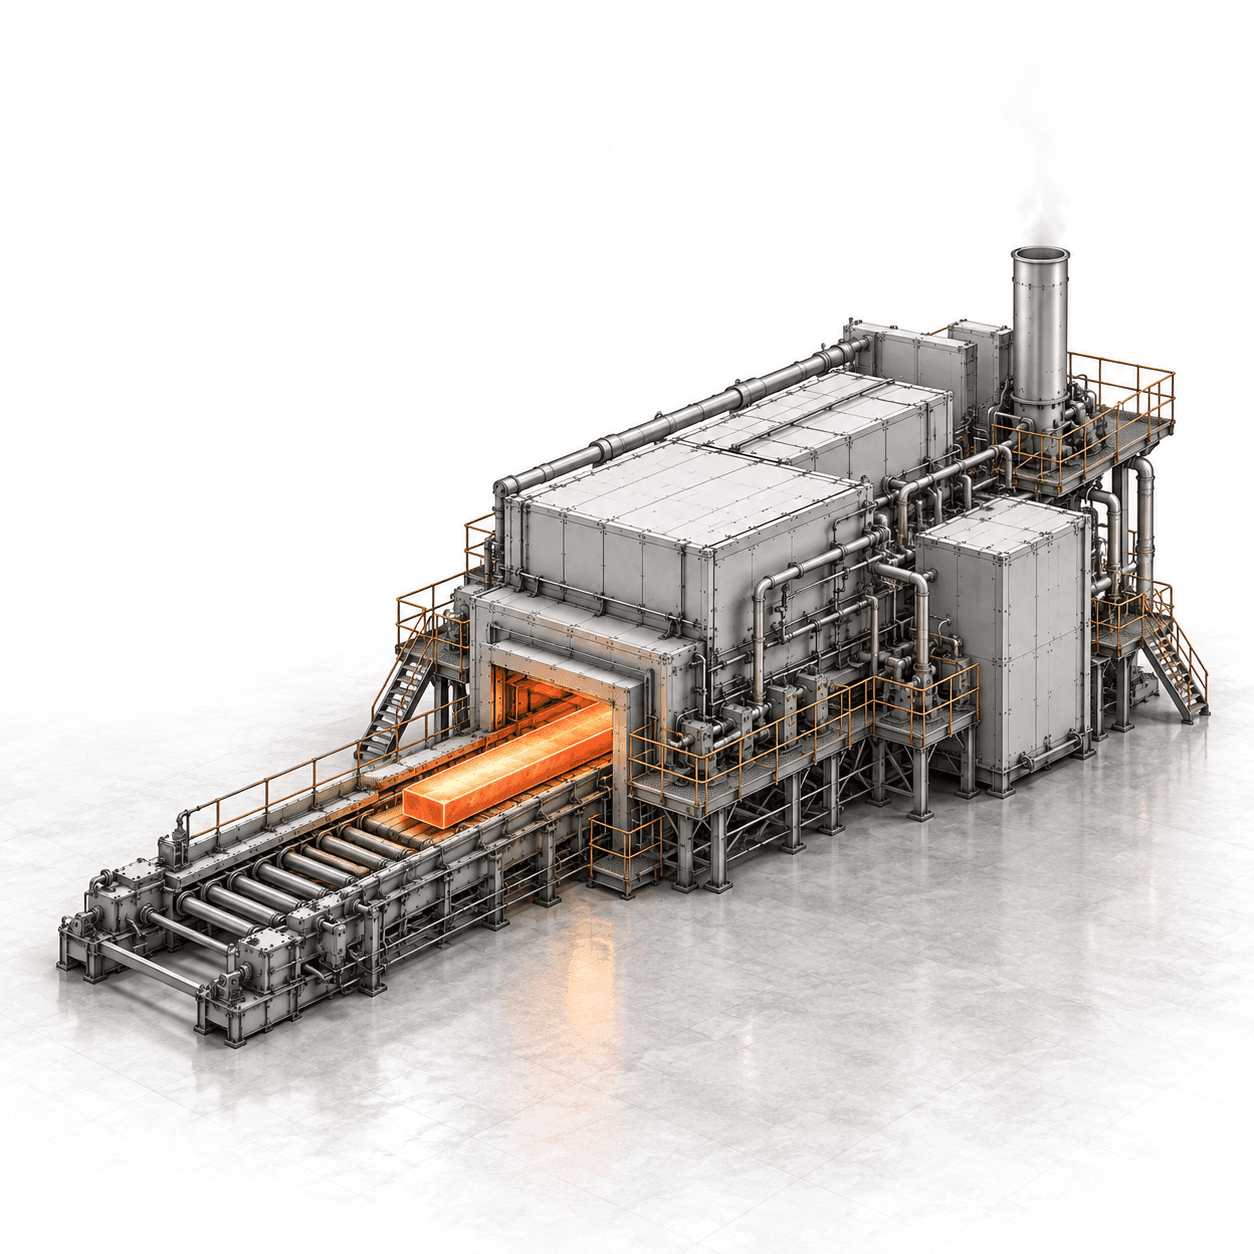
Reheating Process & Soaking
Cast ingots are reheated in gas-fired walking beam furnaces to ensure optimal thermal soaking for hot rolling.
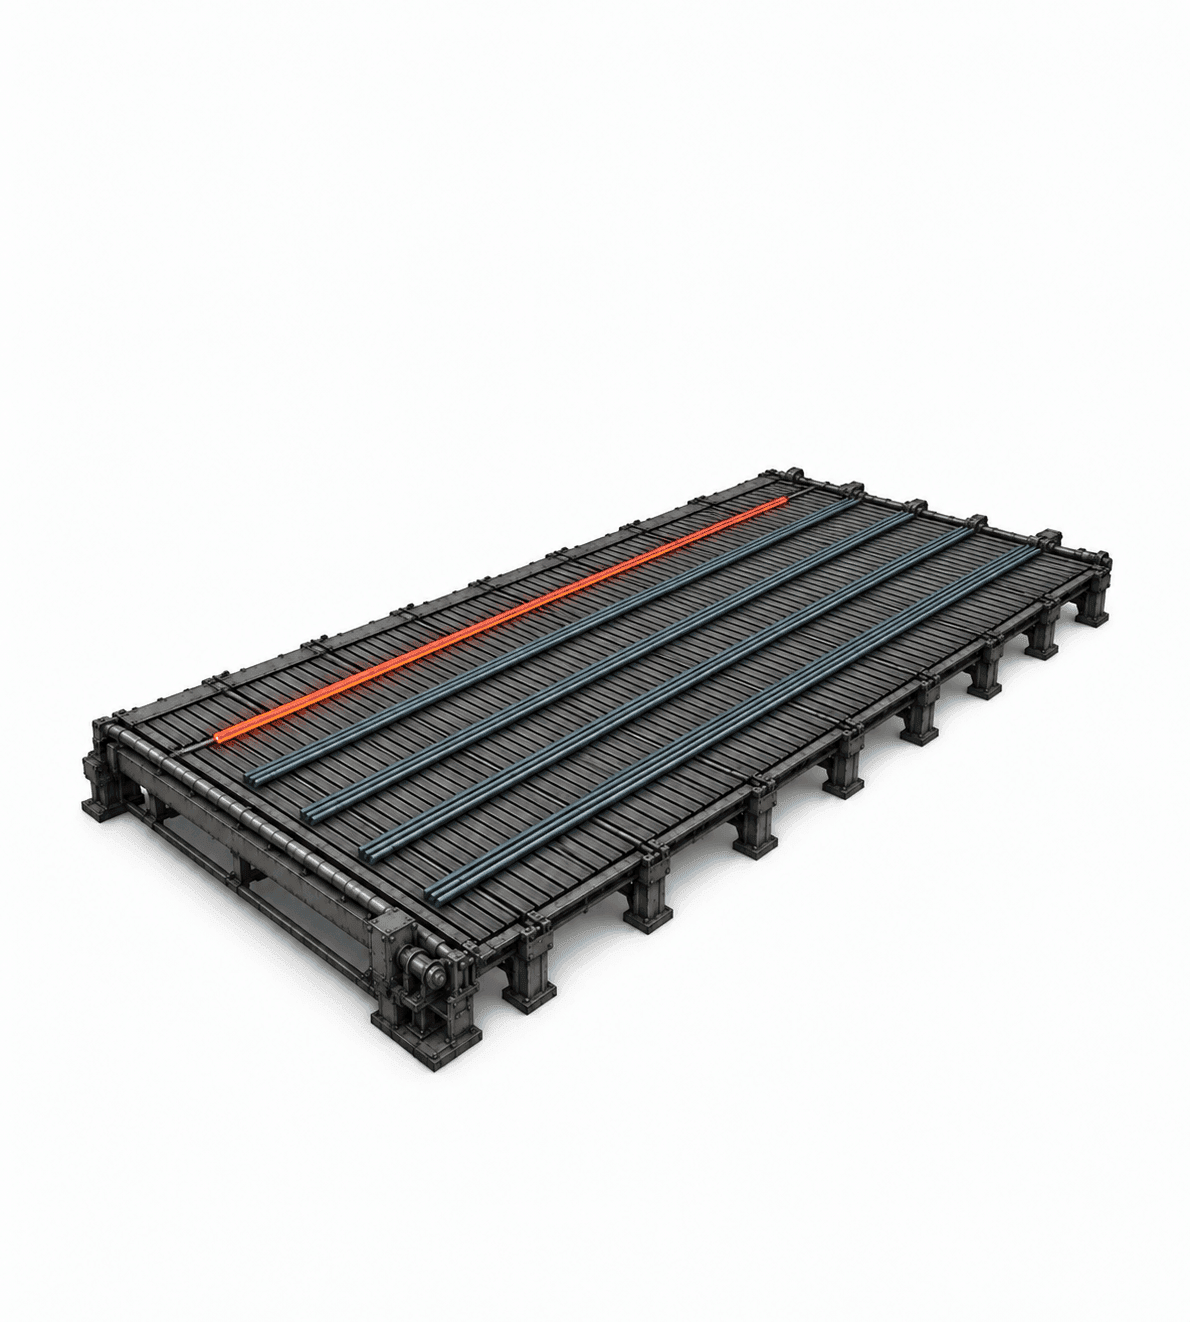
Controlled Cooling Beds
Hot-rolled bars undergo controlled ambient cooling on specialized cooling beds to stabilize material strength.
Cold Finishing Operations
Bars undergo centerless peeling, grinding, and straightening to achieve h9, h11, h12 tolerances and fine surface finish.
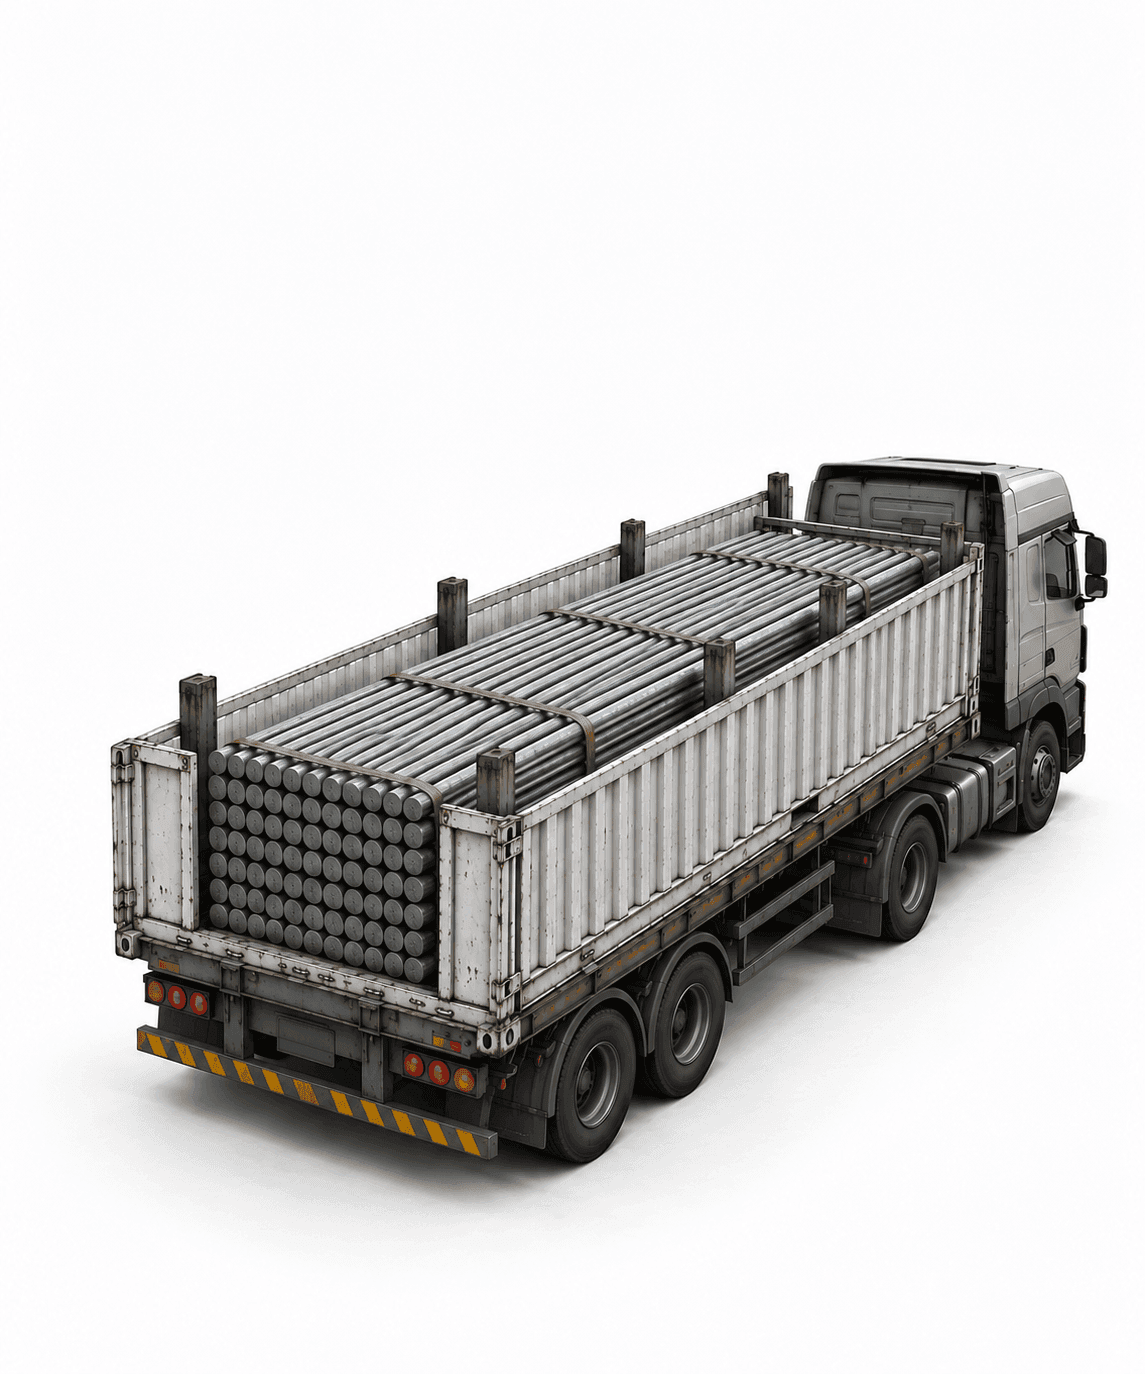
Packing, Marking & Dispatch
Finished products are color coded, bundle tagged, securely packed, and dispatched with Mill Test Certificates (MTC 3.1).
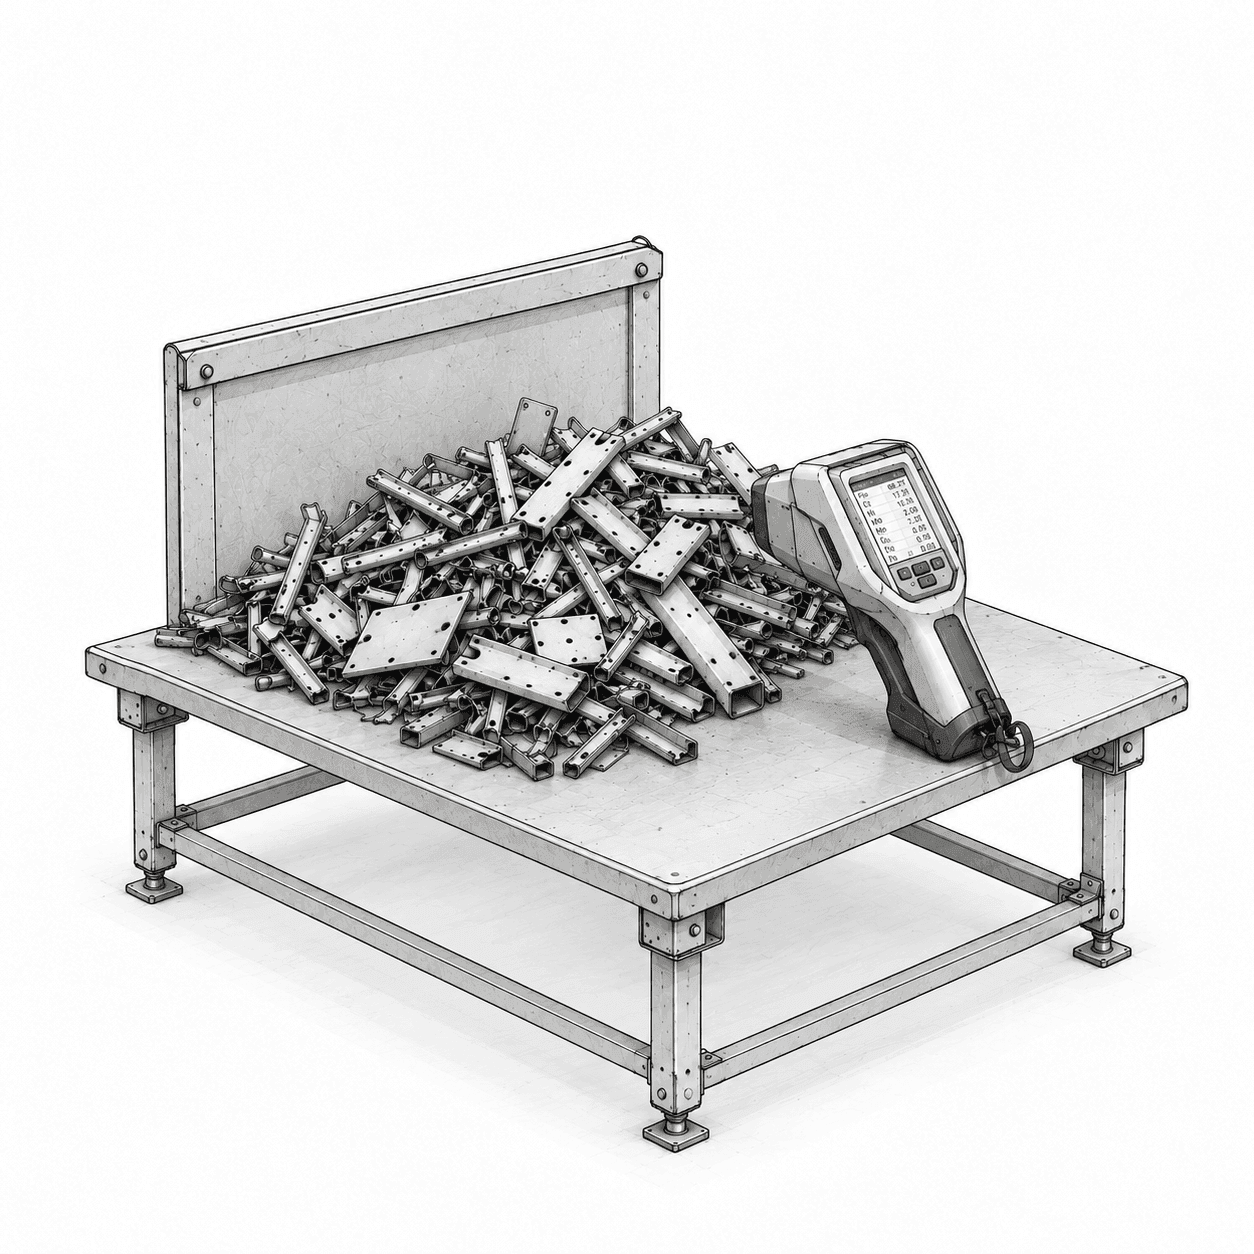
Material Sorting & Spectro Analysis
Raw materials are verified using handheld PMI and Optical Emission Spectrometers to ensure exact alloy chemistry.
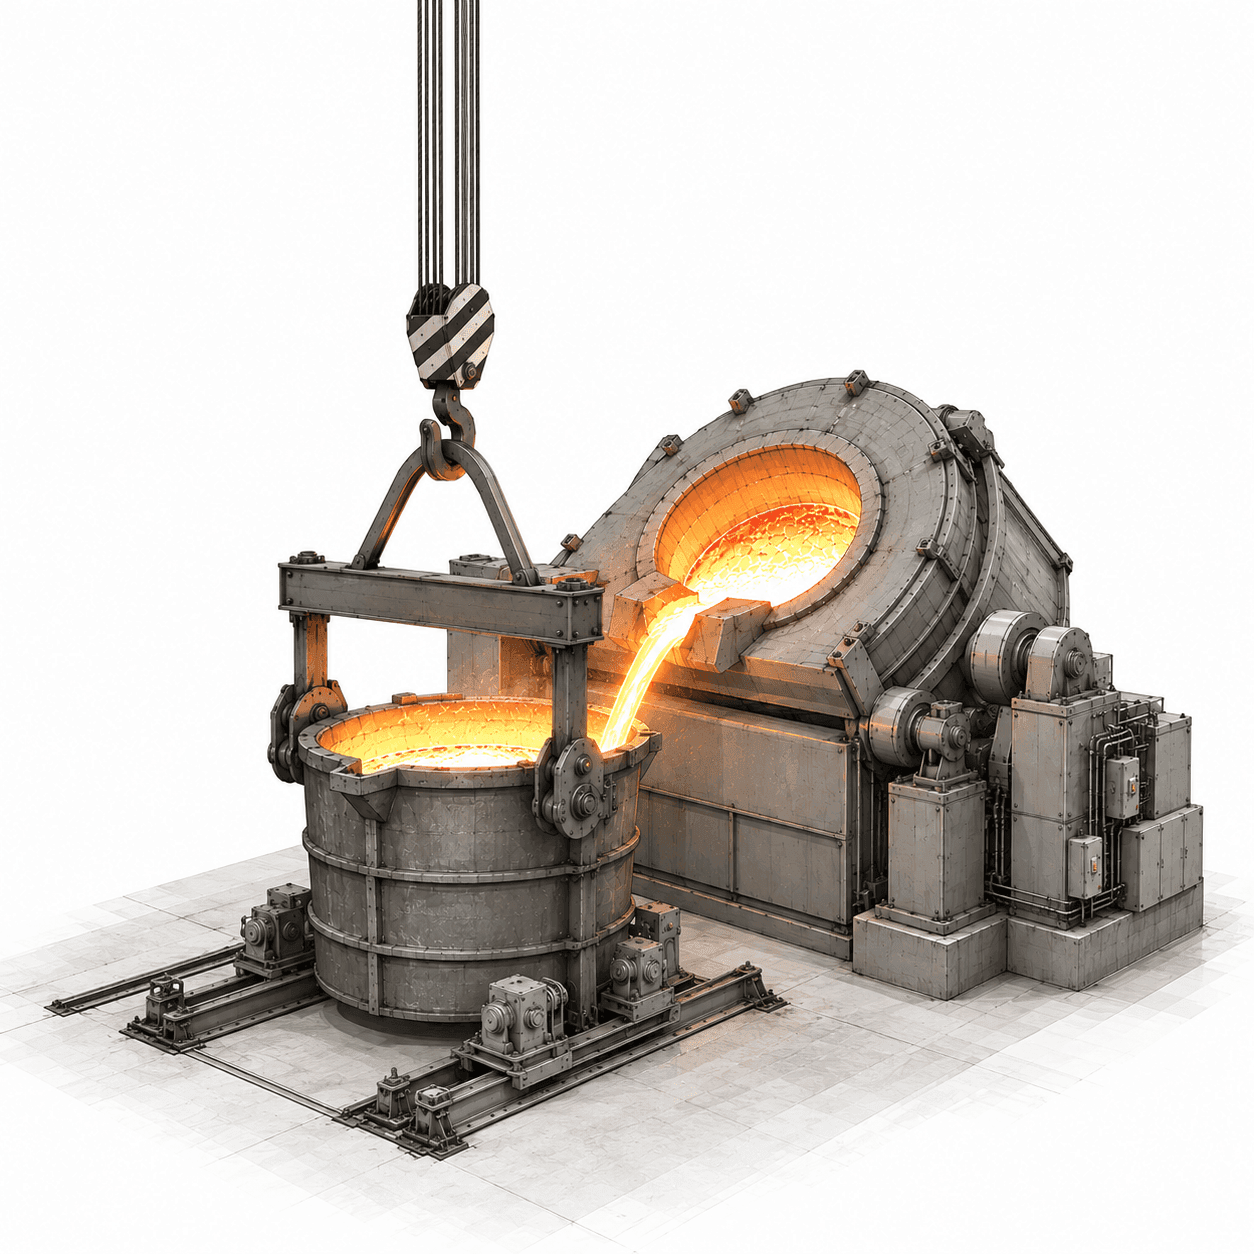
Ladle Refining
Molten steel undergoes controlled ladle refining and gas filtration to optimize alloy chemistry, steel cleanliness, and inclusion control.
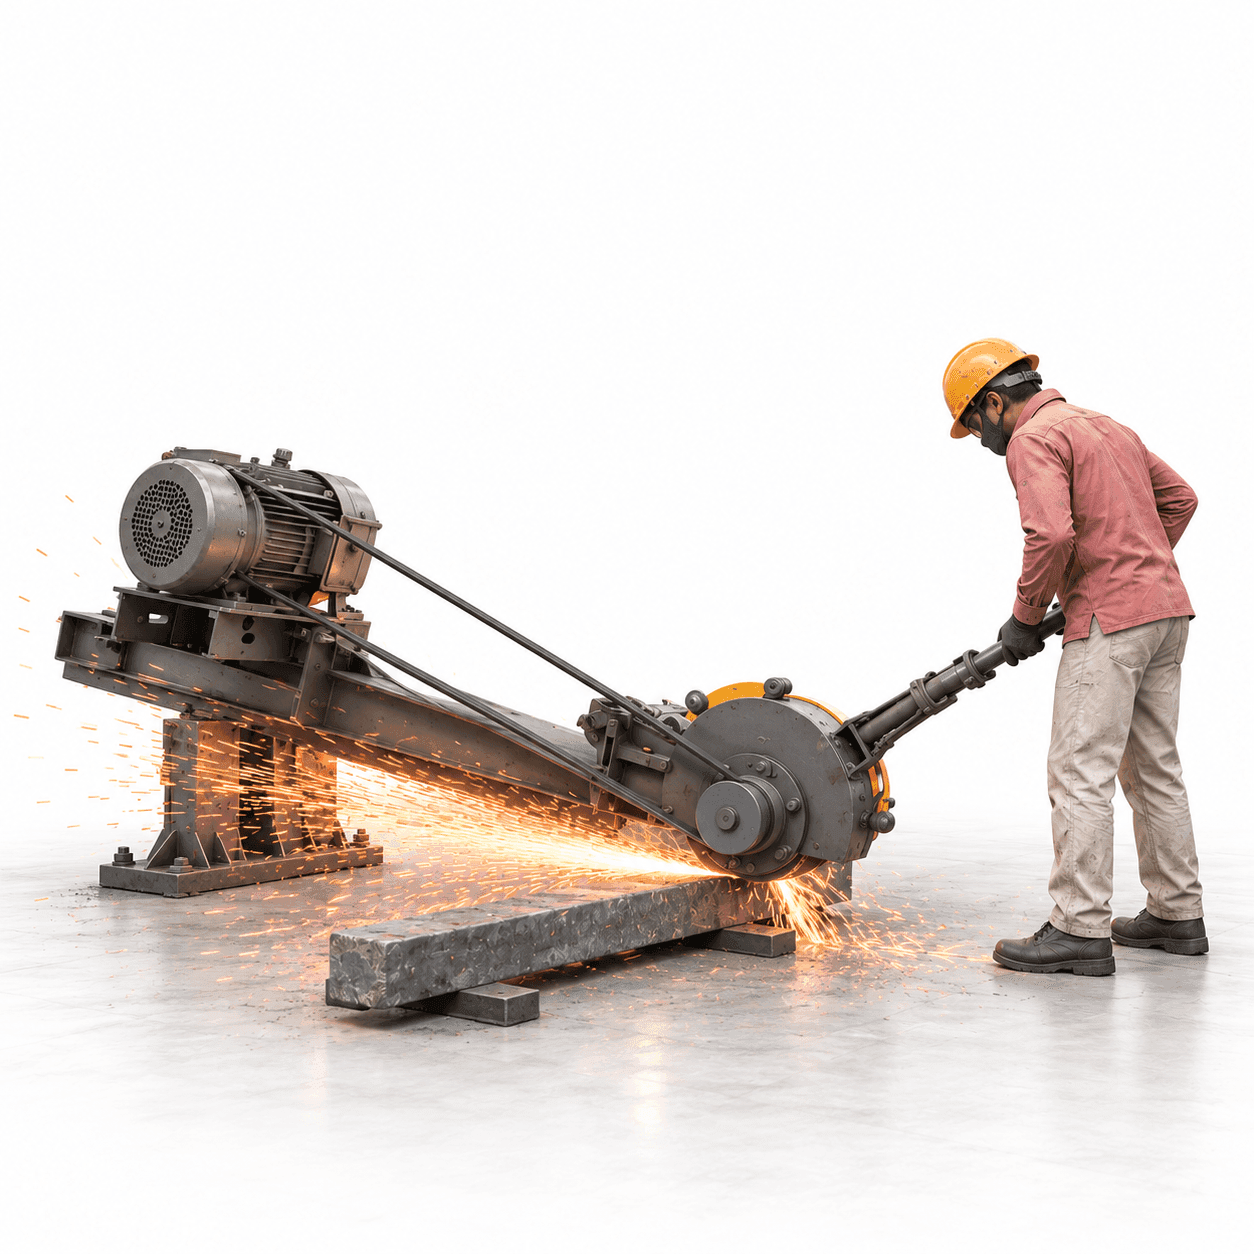
Ingot Grinding & Inspection
Cast ingots undergo 100% surface grinding and thorough inspection to eliminate surface defects prior to rolling.
Hot Rolling Mill
Heated ingots pass through multi-stand rolling lines to form round bars (16mm to 130mm) and RCS with tight accuracy.
Precision Heat Treatment
Products undergo customized heat treatment cycles including Annealing, Hardening, and Tempering per specifications.
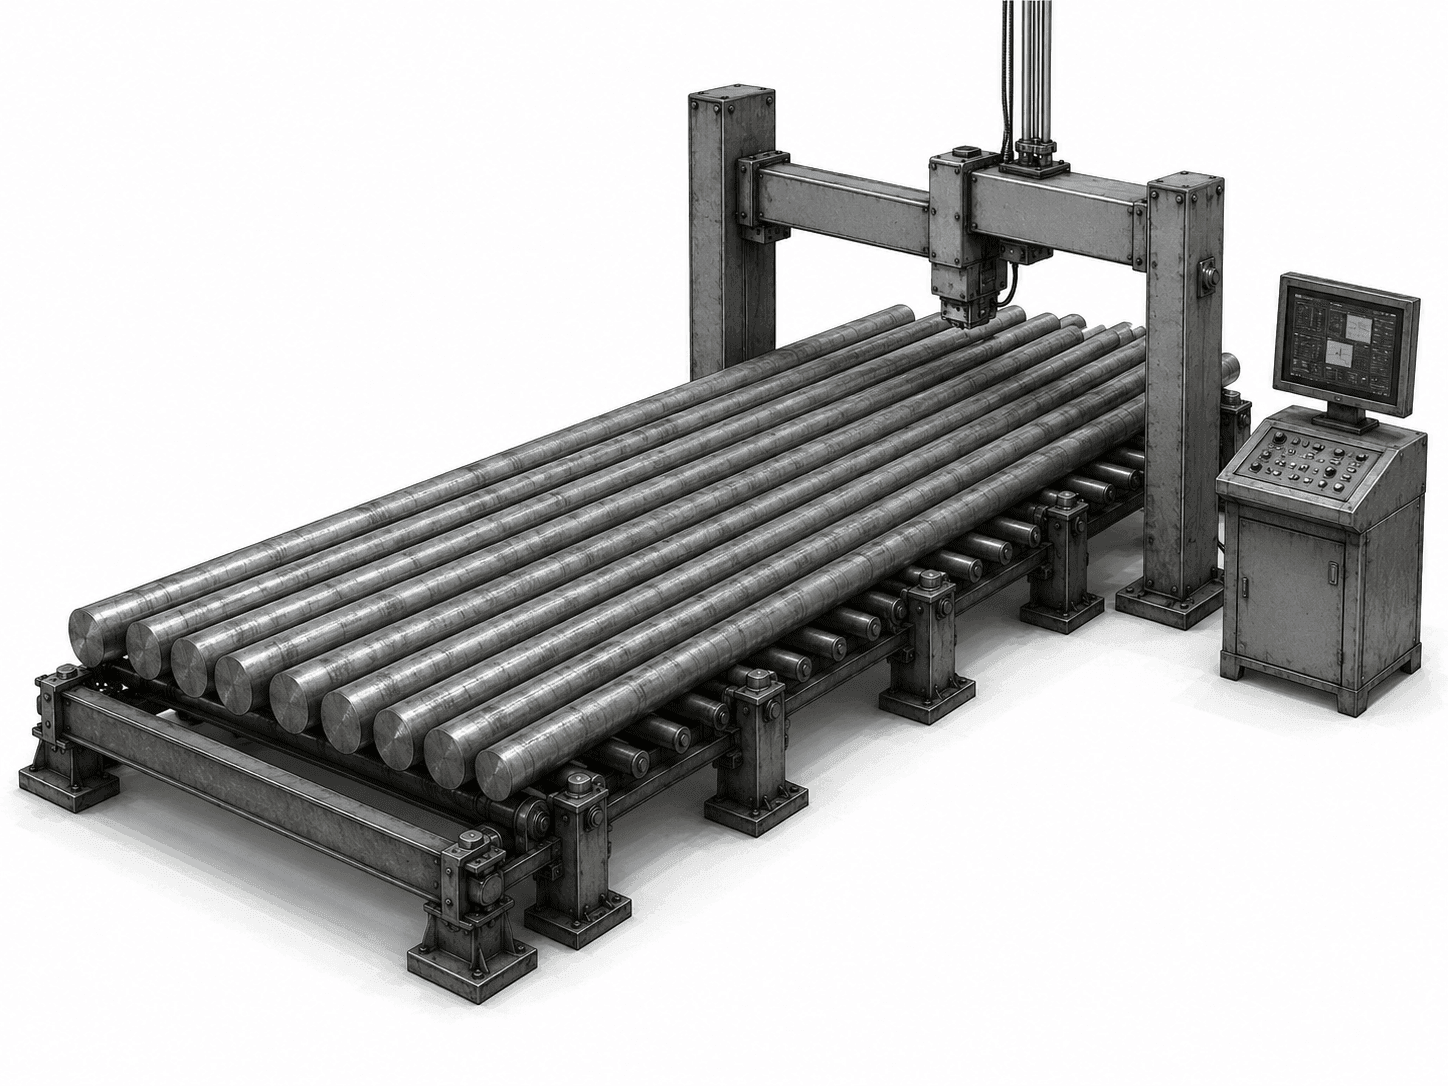
Comprehensive Final Inspection & NDT
Finished products undergo Immersion Ultrasonic Testing (UT), Magnetic Particle Inspection (MPI), and surface audits.
OUR MANUFACTURING PROCESS
A well-defined 13-stage metallurgical process engineered to deliver high-quality alloy steel products.
Raw Material Selection & Audit
High-grade stainless steel scrap and alloy additions undergo strict grade verification prior to furnace charging.
Material Sorting & Spectro Analysis
Raw materials are verified using handheld PMI and Optical Emission Spectrometers to ensure exact alloy chemistry.
Electric Induction Furnace Melting
Selected raw materials are melted under computer-monitored operating parameters and precise pyrometry control.
Ladle Refining
Molten steel undergoes controlled ladle refining and gas filtration to optimize alloy chemistry, steel cleanliness, and inclusion control.
Bottom-Poured Ingot Casting
Refined molten metal is cast into molds under controlled bottom-pouring conditions for uniform grain structure.
Ingot Grinding & Inspection
Cast ingots undergo 100% surface grinding and thorough inspection to eliminate surface defects prior to rolling.
Reheating Process & Soaking
Cast ingots are reheated in gas-fired walking beam furnaces to ensure optimal thermal soaking for hot rolling.
Hot Rolling Mill
Heated ingots pass through multi-stand rolling lines to form round bars (16mm to 130mm) and RCS with tight accuracy.
Controlled Cooling Beds
Hot-rolled bars undergo controlled ambient cooling on specialized cooling beds to stabilize material strength.
Precision Heat Treatment
Products undergo customized heat treatment cycles including Annealing, Hardening, and Tempering per specifications.
Cold Finishing Operations
Bars undergo centerless peeling, grinding, and straightening to achieve h9, h11, h12 tolerances and fine surface finish.
Comprehensive Final Inspection & NDT
Finished products undergo Immersion Ultrasonic Testing (UT), Magnetic Particle Inspection (MPI), and surface audits.
Packing, Marking & Dispatch
Finished products are color coded, bundle tagged, securely packed, and dispatched with Mill Test Certificates (MTC 3.1).
MULTI-STAGE
QUALITY CONTROL
MATRIX.
From raw material spectral analysis to final immersion ultrasonic testing, every heat batch undergoes 6 mandatory quality gates ensuring 100% compliance with international standards.
RAW MATERIAL INSPECTION
Sourced scrap, virgin metals, and alloy additions verified for chemical composition, material grade, physical properties, and heat traceability documentation.
IN-PROCESS INSPECTION
Continuous quality monitoring during cutting, melting, rolling, and machining stages with optical pyrometry and dimensional checks.
HEAT TREATMENT MONITORING
Controlled heating cycles, digital pyrometry temperature logging, controlled cooling, and process documentation ensuring optimal hardness and strength.
MECHANICAL TESTING
Universal Tensile Testing Machine (UTM) testing for tensile strength, 0.2% yield stress, elongation %, impact toughness, Jominy end-quench test, and Brinell/Rockwell hardness.
NON-DESTRUCTIVE TESTING (NDT)
100% Volumetric Immersion Ultrasonic Testing (UT) for internal soundness and Magnetic Particle Inspection (MPI) for surface flaw clearance.
FINAL INSPECTION & CERTIFICATION
Comprehensive final audit of dimensional tolerances (h9-h12), surface finish Ra, color-code identification, protective packing, and MTC EN 10204 3.1 issuance.
IN-HOUSE
METALLURGICAL
TESTING FACILITIES
& EQUIPMENT
Our in-house analytical testing laboratory is equipped with advanced testing systems and experienced professionals to ensure the chemical and mechanical reliability of every heat batch we produce.
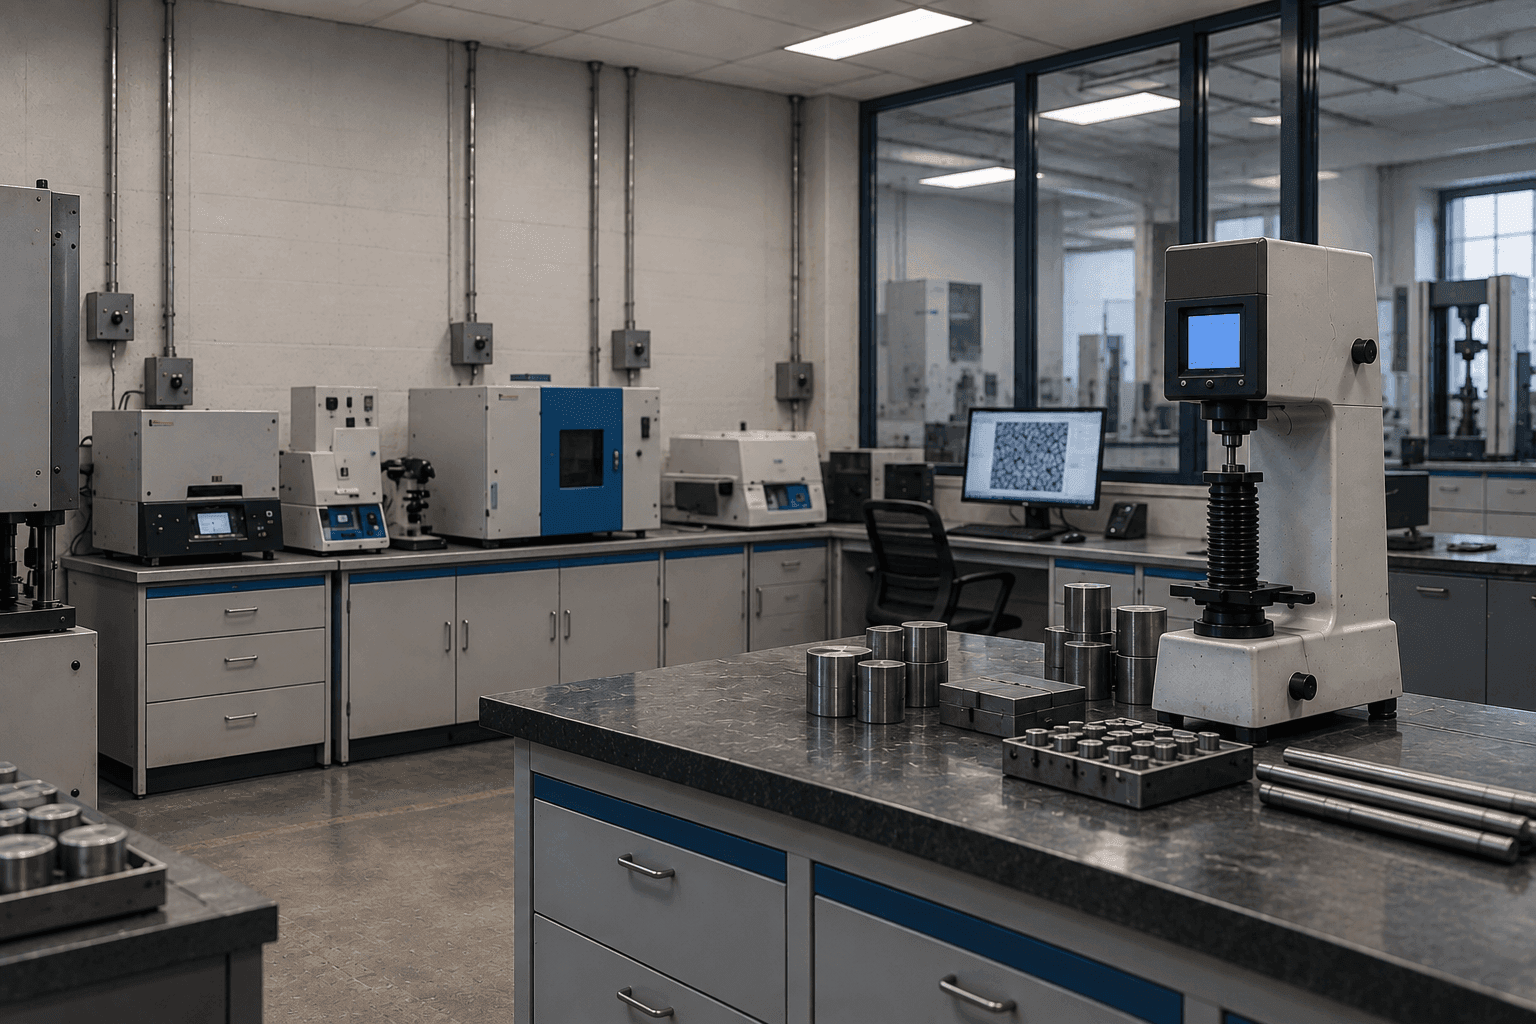
CHEMICAL TESTING DIVISION
Quantitative spectral chemical composition, on-site PMI verification, and microscopic examination.
MECHANICAL & NDT TESTING DIVISION
Destructive mechanical testing, Jominy end-quench hardenability verification, and non-destructive inspection including UT and MPI.
Optical Emission Spectrometer (OES)
High-precision multi-element chemical composition analysis & trace element verification (20+ elements)
Handheld PMI (Positive Material Identification) Gun
Rapid on-site XRF elemental analysis for 100% material grade verification and alloy chemistry confirmation
Optical Metallurgical Microscope
Microstructural examination for grain size measurement, phase identification, and non-metallic inclusion rating
Magnetic Particle Inspection (MPI) System
High-sensitivity electromagnetic crack detection for critical surface and near-surface flaw clearance
Immersion Type Ultrasonic Testing (UT)
Volumetric immersion ultrasonic wave scanning for internal soundness free of voids and flaws
Universal Tensile & Jominy Testing Setup
Tensile strength, 0.2% yield stress, elongation %, and Jominy end-quench hardenability curve verification
RESPONSIBLE OPERATIONS
OUR COMMITMENT.
BEYOND TODAY.
We continuously evolve our technology, processes and people to deliver superior quality with responsibility and care.
CONTINUOUS IMPROVEMENT
Driven by innovation and a future-ready mindset, we continuously invest in people, processes and technology to stay ahead.
RESPONSIBLE OPERATIONS
Safety, reliability and sustainability are at the core of our operations.
STANDS APART.
ADVANCED
FACILITY
State-of-the-art infrastructure built for precision, efficiency and consistent quality.
SUPERIOR
MANUFACTURING
Advanced melting, rolling and heat treatment technology to deliver superior performance.
QUALITY
ASSURANCE
Rigorous inspections and advanced in-house testing ensure flawless quality at every stage.
STRICT PROCESS
CONTROL
Systematic process control and traceability from raw material to final dispatch.
HIGH PRODUCTION
EFFICIENCY
Optimized processes and modern equipment ensure consistent output and on-time delivery.
GLOBAL STANDARD
COMPLIANCE
Manufacturing and quality systems aligned with national and international standards.
DISCOVER OUR CAPABILITIES.
GET IN TOUCH WITH US
Have custom steel specifications or technical inquiries? Connect with our team today.